Complete PET line planning
PET Water Bottling Line: From Preform to Finished Pack
Plan the complete PET bottle-to-pallet workflow before comparing machines. Define bottle supply, blowing, filling, labeling, packing, utilities, line balance, factory interfaces and supplier responsibility as one coordinated production system.
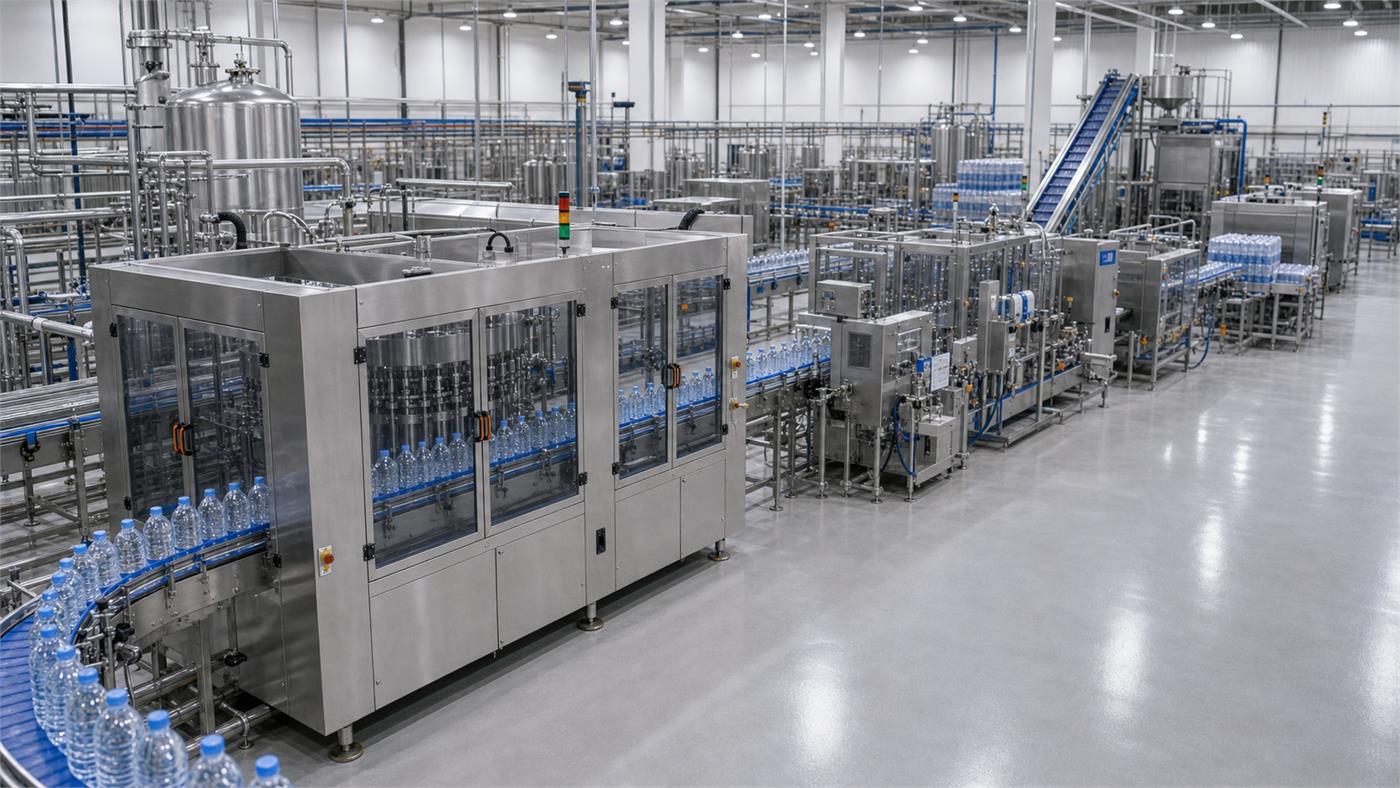
A PET Bottling Line Is More Than a Filling Machine
A complete PET water bottling line connects every step that turns treated water and packaging materials into stable, identified and packed finished goods. The project should be planned around one approved bottle family, product specification, pack route and acceptance basis.
- Bottle or preform supply route
- Rinsing, filling and capping center
- Labeling, coding and finished pack
- Utilities, controls and supplier interfaces
What a Complete PET Water Bottling Line Includes
The exact equipment list depends on the approved bottle, water product, output target and factory conditions. These systems should be discussed together even when different suppliers provide them.
Water treatment interface
The line needs an agreed treated-water specification, storage and delivery route. Raw-water treatment design remains a separate process decision that must match the filling demand.
PET bottle supply
Choose purchased empty bottles, an in-house blower or an integrated blow-fill architecture. Preforms, molds, storage and bottle transfer change with that choice.
Bottle blowing and feeding
When bottles are made on site, confirm preform handling, heating, molds, compressor, dryer, cooling and the transfer route into the filling center.
Rinsing, filling and capping
The main machine must match the approved water product, bottle drawings, neck finish, cap samples, output basis and sanitation procedure.
Labeling and coding
Label type, label material, code location, inspection access and changeover parts should be confirmed from approved samples.
Secondary packing
Define film pack, tray, carton or another approved retail format. Packing output and pack stability must be considered in the balanced line.
Conveyors and coordinated controls
Bottle and pack conveyors need suitable transfer, accumulation, rejection points and control signals between machines.
Finished-goods movement
Pallet preparation, warehouse routes, loading access and operator handling should be planned so packing does not create the final bottleneck.
Choose the PET Line Architecture Before Requesting Price
There is no universal best configuration. The right architecture depends on bottle supply, output, factory space, utilities, maintenance capability and future plans.
| Architecture | Suitable planning context | Items that still need confirmation |
|---|---|---|
| Purchased bottles plus filling line | A practical startup route when approved empty bottles are available locally and bottle logistics are manageable. | Bottle quality, storage hygiene, unscrambling or feeding, transport damage, supplier continuity and the future change to in-house blowing. |
| Standalone blower plus filler | Useful when the plant wants bottle control while keeping bottle blowing and filling as separate machines. | Preforms, molds, compressor, cooling, air conveyor, accumulation, floor space, line controls and operator responsibilities. |
| Integrated blow-fill-cap block | A compact connected architecture for projects whose bottle family, utilities, maintenance skills and output requirements support integration. | Approved preforms and bottles, molds, air and cooling systems, cleaning, changeover, downstream packing and lifecycle support. |
Convert Bottle Speed Into the Pack Rate You Need
Check the bottle and pack stages in their own units. A filler may be quoted in bottles per hour while the packer is quoted in packs per minute. Convert them using the actual bottle count per pack before judging whether the equipment can run together.
| Planning check | Example or method | Meaning for the purchase |
|---|---|---|
| Convert the pack rate | Illustrative arithmetic: 5,000 bottles/hour divided by 12 bottles/pack is 416.7 packs/hour, or about 6.94 packs/minute. | This is a conversion example, not a model rating or recommended design margin. The supplier must establish required sustained capacity under the agreed conditions. |
| Account for pack changes | At the same bottle output, a six-bottle pack needs twice as many packs per minute as a twelve-bottle pack. | A packer suitable for one format may limit another. Include each launch pack in the balance table. |
| Use one loss definition | Separate rated speed from accepted output and define planned stops, rejects and changeovers once. | Do not apply a second downtime factor to hours that already exclude the same stops. Keep assumptions consistent with the existing capacity planner. |
| Check every transfer | Compare bottle supply, filling, labeling, coding, accumulation, pack discharge and pallet movement for the same SKU. | An isolated fast filler cannot compensate for a slower dry end. Accumulation can absorb short interruptions but cannot fix a persistent capacity deficit. |
For purchased bottles, record the feed method and refill interruptions. For in-house blowing, add the reference preform, bottle mold, blowing air, cooling and bottle-transfer basis. Do not transfer a rated performance figure from a different bottle shape or material without confirmation.
Request a line-balance schedule with one row per launch SKU and one column per machine. It should identify the expected limiting stage and how a short stop is recovered. Test the connected production route with the agreed bottles, caps, labels and packaging materials.
Information to Send for a PET Bottling Line Proposal
A detailed buyer brief gives suppliers a common basis and makes technical and commercial comparisons more meaningful.
| Brief section | Information to provide | What the supplier should return |
|---|---|---|
| Water product | Still or sparkling product, source-water information and available treatment basis. | Confirmed product application, treatment interface and any limitations or open questions. |
| Bottle and preform | Bottle drawings or samples, neck finish, weight, launch sizes and preform plan when blowing is included. | Approved range, molds and change parts, bottle handling route and sample requirements. |
| Cap, label and code | Cap samples, label type and dimensions, code content and intended code position. | Cap feeding scope, labeler and coder selection, change parts and approval procedure. |
| Finished pack | Film, tray, carton or mixed format with pack arrangement and material samples when available. | Packing machine scope, conveyor interfaces, material assumptions and pack test plan. |
| Output and schedule | Target output by bottle size, shifts, product changes and expected future formats. | Rated basis for each format, balanced-line assumptions, changeover scope and identified bottlenecks. |
| Factory and utilities | Floor sketch, doors, columns, ceiling, drains, room limits, power and utility conditions. | Preliminary layout, connection schedule, buyer-side works and unresolved site requirements. |
| Acceptance basis | Available samples, desired FAT evidence, documents, training and installation expectations. | FAT protocol, document list, service boundary, open-item process and handover scope. |
Questions That Prevent Scope Gaps Between Machines
Many PET line problems occur at the interfaces rather than inside one machine. Put these questions into the technical review before purchase.
Treatment to filler
Who specifies treated-water pressure, quality, buffer storage, piping, cleaning and the final connection to the filling center?
Blower to filler
Is bottle transfer by air conveyor, floor conveyor or integrated connection, and who owns bottle stability at the transfer?
Cap supply
Are cap elevator, sorter, chute, change parts, rejected-cap handling and approved cap samples included?
Filler to labeler
Are discharge conveyor, bottle spacing, drying, inspection and accumulation defined for the chosen label process?
Labeler to packer
Can conveyors and controls manage rejected bottles, code checks, pack grouping and short downstream stops?
Packer to warehouse
Who supplies pack conveyors, pallet preparation and final transfer, and what remains manual at startup?
Machine-to-machine controls
Which signals, safety interlocks, stop logic, alarms and communication responsibilities cross supplier boundaries?
Installation ownership
Mark unloading, positioning, leveling, electrical work, piping, consumables, commissioning support and acceptance as supplier or buyer tasks.
Documents and Evidence to Review Before Shipment
A professional PET water bottling line project should move through documented approval gates. The exact tests must be agreed for the purchased scope and supplied samples.
Approved equipment scope
A line-by-line list of included, optional, excluded and buyer-supplied items prevents the commercial title from hiding omissions.
Bottle and packaging approvals
Keep approved bottle, preform, cap, label and pack drawings or samples linked to each machine that handles them.
Layout and access drawing
Review line direction, operator aisles, maintenance access, doors, columns, drains, utility drops and future expansion space.
Utility connection schedule
Use supplier-specific connection requirements for power, air, cooling, water, drains and ventilation rather than generic estimates.
Interface responsibility list
Identify ownership for conveyors, signals, pipe connections, cap supply, coding, inspection and all transitions between systems.
FAT protocol
Agree supplied materials, run conditions, observations, measurements, safety checks, documents and treatment of open items.
Spares, manuals and training
Confirm wear parts, critical spares, tools, manuals, electrical documents, maintenance instructions and operator training scope.
Open-item and handover record
Unresolved work should have an owner, evidence requirement and closure route before shipment, installation or final acceptance.
Freeze the Packaging References Across the PET Line
Use one controlled package record from bottle supply through finished pack. This prevents the blower, filler, capper and packer from quoting against different versions of what appears to be the same bottle. A later packaging change should identify every affected station.
| Packaging reference | Equipment that needs it | Change-review trigger |
|---|---|---|
| Preform and bottle drawing | Blower or purchased-bottle supply; empty-bottle transport and filler | New bottle body, neck, weight or approved preform |
| Neck and closure pair | Neck handling, cap feeder and capper | Changed neck finish, cap product reference or closure geometry |
| Filled-bottle geometry and label | Discharge conveyors, inspection, labeler and coder | Changed height, body profile, label panel or code location |
| Finished pack specification | Grouping, film/tray/carton packing and pack transport | Changed bottles per pack, arrangement or pack material |
FAQ
What is a PET water bottling line?
A PET water bottling line connects bottle supply, rinsing, filling, capping, labeling, coding, packing and conveying for water packed in PET bottles. A complete plant may also include water treatment, utilities, inspection, warehouse handling and startup support.
What equipment should a complete PET bottling line include?
Confirm preform feeding and blowing or empty-bottle feeding, air conveyor, rinsing filling capping, cap handling, labeling, coding, bottle and pack conveyors, packing, inspection, controls, startup spares and documentation. Treatment and utilities should be listed as included or buyer-side.
Should PET blowing and filling use separate machines or an integrated block?
Both architectures can be appropriate. Separate machines can offer flexible layout and independent service access, while an integrated blow-fill-cap block reduces empty-bottle transfer. Compare bottle range, output, hygiene, utilities, maintenance skills, footprint and upgrade plans.
Can one PET water bottling line handle several bottle sizes?
A supplier can review a defined bottle family, but volume alone is not enough. Neck finish, height, diameter, shape, weight, base stability, label panel, cap and pack format affect blowing, transfer, filling, labeling and packing.
Should a startup PET line buy empty bottles or blow bottles in-house?
Purchased bottles can simplify the first stage when local supply is reliable. In-house blowing adds preform control and reduces empty-bottle logistics, but it also requires molds, high-pressure air, cooling, space, operators and maintenance.
How should PET line capacity be balanced?
Use one approved bottle and production basis, then check treatment, bottle supply, filling, labeling, packing, accumulation and warehouse movement against the same target. The slowest recurring section can limit real line output.
What utilities does a PET water bottling line require?
Depending on scope, the plant can require incoming water, treated water, power, low-pressure air, high-pressure air for blowing, cooling, drainage and ventilation. Final values must come from the approved equipment and operating basis.
What samples should be approved before a PET line quotation?
Provide bottle or preform drawings and samples, neck finish, cap, label artwork and material, date-code position, film or carton details and the finished pack pattern. Mark future formats separately from launch formats.
Can the same PET bottling line run still and sparkling water?
Do not assume full compatibility. Filling method, pressure handling, bottle design, product preparation, cleaning and controls can differ. Ask the supplier to identify shared modules, product-specific modules and the approved test basis.
What should be verified during FAT for a PET bottling line?
Agree the bottle, cap, label, pack materials, run conditions, measurements and responsibility boundaries before testing. Review safety, interfaces, line balance, rejects, changeovers, documents, spares and an open-item list before shipment.
Request a PET Water Bottling Line Scope Review
Share what you know now. The goal is to prepare a useful plant brief before a machine quotation is built.