utilities planning question
How should high- and low-pressure air be separated for PET blowing?
PET blowing and general machine air can use different pressure and quality duties. Map compressors, treatment, receivers, recovery, distribution, pressure drops, isolation and fallback from supplier-specific demand data.
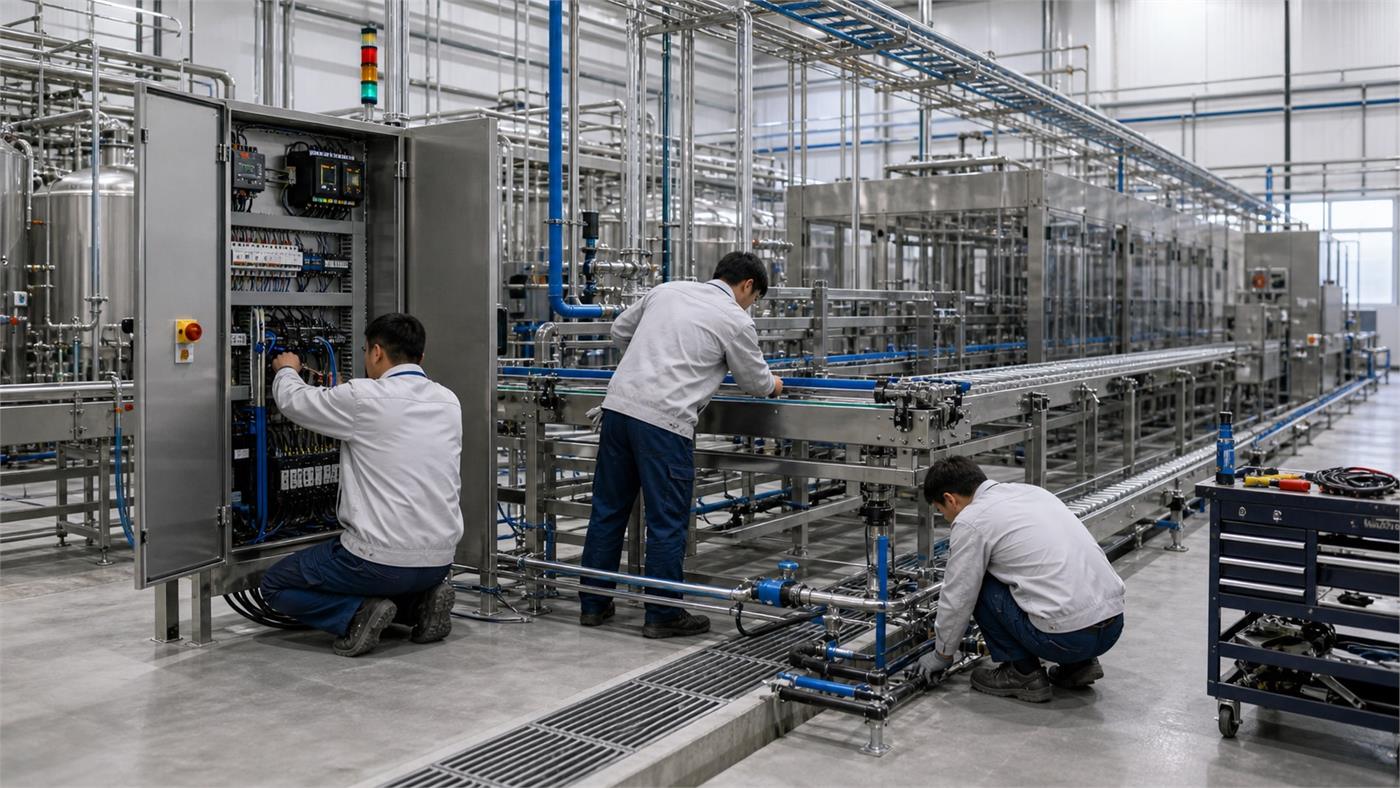
High- and Low-Pressure Air Network for PET Blowing
PET blowing and general machine air can use different pressure and quality duties. Map compressors, treatment, receivers, recovery, distribution, pressure drops, isolation and fallback from supplier-specific demand data. Use the checklist below to turn the question into a supplier-ready decision without relying on universal figures or unverified claims.
- Blower model and bottles
- Other air consumers
- Plant layout
- Redundancy objective
Decisions Behind High- and Low-Pressure Air Network for PET Blowing
Define these items against the real product, package, site and production plan before comparing equipment or supplier proposals.
Consumer separation
List high- and low-pressure duties
Generation
Define compressors, dryers and filters
Distribution
Size routes from actual demand and pressure loss
Resilience
Plan isolation, storage and contingency
High- and Low-Pressure Air Network for PET Blowing Supplier Evidence Matrix
Use the matrix to separate buyer inputs, supplier commitments and evidence that can be checked during design review, FAT, installation or operation.
| Decision | What to define | Evidence to request |
|---|---|---|
| Consumer separation | List high- and low-pressure duties | Air-flow and pressure diagram |
| Generation | Define compressors, dryers and filters | Supplier demand curves |
| Distribution | Size routes from actual demand and pressure loss | Pipe network calculation |
| Resilience | Plan isolation, storage and contingency | Control and fallback narrative |
Project Inputs for High- and Low-Pressure Air Network for PET Blowing
Incomplete inputs force suppliers to make assumptions. Mark unknown items openly and assign the next action instead of hiding the gap.
Blower model and bottles
Provide current, project-specific information for PET blowing air network so the supplier can state assumptions and remaining decisions.
Other air consumers
Provide current, project-specific information for PET blowing air network so the supplier can state assumptions and remaining decisions.
Plant layout
Provide current, project-specific information for PET blowing air network so the supplier can state assumptions and remaining decisions.
Redundancy objective
Provide current, project-specific information for PET blowing air network so the supplier can state assumptions and remaining decisions.
FAQ
How should high- and low-pressure air be separated for PET blowing?
PET blowing and general machine air can use different pressure and quality duties. Map compressors, treatment, receivers, recovery, distribution, pressure drops, isolation and fallback from supplier-specific demand data.
Which inputs are needed for PET blowing air network?
Start with Blower model and bottles, Other air consumers, Plant layout, Redundancy objective. The selected supplier and qualified local specialists must confirm the final project basis.
What evidence should a supplier provide for PET blowing air network?
Request Air-flow and pressure diagram, Supplier demand curves, Pipe network calculation, Control and fallback narrative. Compare evidence against the same approved product, package, capacity and site conditions.
What is a common mistake when planning PET blowing air network?
A common mistake is accepting a generic answer without defining the actual bottle, product, output, utilities, interfaces and acceptance method for the project.
How does PET blowing air network connect to a complete water bottling line?
It affects adjacent equipment, controls, utilities, layout, quality checks or operating responsibilities. Record those interfaces in the complete-line scope and responsibility matrix.
Find a specific operating problem
Planning calculator: PET blowing air demand
Enter measured or explicitly assumed values. Keep the units and measurement boundary consistent. Compare a second scenario before choosing equipment.
Equation and scope
A × B ÷ 60
- A: Reference air per bottle [L (reference conditions)]
- B: Bottle rate [Bottles/h]
⌈x⌉ rounds upward and ⌊x⌋ downward to a whole count. min/max select the lowest/highest sample. ∉ means outside the stated interval.
Calculate reference-condition air demand from air use per bottle and bottle rate. Do not compare reference litres with compressed pipe litres. Blowing and control networks still require their own pressure, quality and peak-flow specifications.
Worked example: editable assumptions
Record assumptions separately from measurements. The example numbers demonstrate arithmetic and are not a recommended equipment specification.
| Input or result | Value | Unit |
|---|---|---|
| A — Reference air per bottle | 12 | L (reference conditions) |
| B — Bottle rate | 6000 | Bottles/h |
| Flow | 1200 | L/min (reference conditions) |
Your project inputs
Calculated result
| Input or result | Value | Unit |
|---|---|---|
| Flow | 1200 | L/min (reference conditions) |
This is a planning estimate from the stated inputs, not a machine guarantee or design approval.
Calculation stays in this browser; this worksheet sends no project inputs to the server.
Before procurement, ask the responsible specialist to review the assumptions, drawings and test evidence. A valid calculation does not mean a project has passed acceptance.
Why can compressor demand rise without a change in bottle rate?
These are invented teaching inputs, not equipment ratings, market prices or an accepted tolerance. The two scenarios change one assumption while holding the other inputs constant. Use the comparison to identify what must be measured or agreed for your project.
Read both inputs and outputs in the stated units. The input register explains what evidence to request before substituting your own values. If a source is missing, record the uncertainty rather than silently entering zero or accepting a supplier estimate as a measurement.
Changed assumption: Reference air per bottle
Input assumptions
| Record item | Unit | Scenario A | Scenario B |
|---|---|---|---|
| Reference air per bottle | L (reference conditions) | 10 | 14 |
| Bottle rate | Bottles/h | 7,200 | 7,200 |
Calculated comparison
| Record item | Unit | Scenario A | Scenario B |
|---|---|---|---|
| Flow | L/min (reference conditions) | 1,200 | 1,680 |
What the comparison means
The bottle rate is fixed but the assumed reference air use per bottle increases. The calculated demand rises even though the production target is unchanged. This is why comparing only bottles per hour can hide a different preform or bottle recipe. Reference-condition demand must also be kept distinct from the volume occupied in a pressurized pipe.
How to establish this input
| Record item | How to establish this input |
|---|---|
| Reference air per bottle | Retain the material or fluid identity, operating condition, declared reference basis and source for the load, property or dose. Check whether a supplier value is measured, specified or assumed before applying it to the actual process. |
| Bottle rate | Record the quantity or distance and the corresponding observation time, named product format and operating mode. Distinguish a measured rate from a quoted capability; an average across a different window is not the same input. |
Evidence to request
Request measured air use for the named bottle and preform, stated reference conditions, operating window and separate blowing and control-air boundaries. Confirm peak-flow and pressure requirements independently.
Project decision record
| Record item | Project decision record |
|---|---|
| Input assumptions | Identify the bottle, pack or material configuration, operating mode and measurement boundary. State the start and finish of the observation and which accepted output the comparison represents; unlike boundaries cannot establish a performance improvement. |
| How to establish this input | Mark every input as measured, taken from a drawing, quoted or assumed. Retain the source document identifier, revision, date and responsible person. The same numeral with a different unit or data status is not automatically a comparable input. |
| Project decision record | Ask the responsible supplier and buyer to agree actual acceptance criteria and the evidence that will demonstrate them. Teaching values and calculated outputs on this page do not become approved operating settings or contractual performance guarantees. |
| Evidence to request | Record the decision affected by the result, the measurement or trial still needed, its owner and the next review. Keep unresolved items visible in the handover file instead of changing the figures to make a preferred equipment option appear acceptable. |
Why can an air-flow comparison be wrong even with matching numbers?
Air consumption per bottle must use the same declared reference conditions as the supply figure. Changing bottle rate or per-bottle use changes this arithmetic demand independently. A reference-volume estimate does not specify operating pressure, peak demand, air quality or pressure loss; request those items separately.
Which inputs should you verify before using this result?
These are hypothetical sensitivity examples, not measurements from a factory. The lower and higher inputs are chosen for teaching; they are not equipment limits, approved settings, uncertainty intervals or recommended allowances. Whole-count and bounded inputs are adjusted to keep the examples valid, so the changes are not all the same percentage.
Read one input row at a time. For its lower and higher result, only that named input changes; every other input remains at the baseline shown in the first table. Do not combine all the lower columns or all the higher columns into a single operating scenario: those combined conditions have not been calculated here.
Baseline and selected input changes
| Input being changed | Unit | Lower input | Baseline input | Higher input |
|---|---|---|---|---|
| Reference air per bottle | L (reference conditions) | 8 | 10 | 12 |
| Bottle rate | Bottles/h | 5,760 | 7,200 | 8,640 |
Output when one input changes
| Input being changed | Calculated output | Lower input | Baseline input | Higher input |
|---|---|---|---|---|
| Reference air per bottle | Flow (L/min (reference conditions)) | 960 | 1,200 | 1,440 |
| Bottle rate | Flow (L/min (reference conditions)) | 960 | 1,200 | 1,440 |
Interpret this problem
A one-input comparison isolates the arithmetic effect inside this model. It does not establish that the input can change independently on a real line. If two quantities share the same measurement, production period or physical constraint, ask the responsible supplier to review that relationship before changing the project basis.
Equal displayed results need interpretation. Whole-item outputs can remain unchanged until a rounding boundary is crossed; displayed decimal values can also hide a small change. Check the stated unit, the underlying counts and the specific explanation below before concluding that an input has no effect.
What to verify next
Use a surprising difference to choose the next measurement, rather than selecting whichever assumption gives the preferred answer. Record the input label and unit, its measured or assumed status, document revision, operating condition and who will verify it. Keep the original record so a later reader can reproduce the comparison.
For a supplier discussion, take the baseline, one changed input, the affected output and the unresolved question together. Agree the field observation or controlled trial that can resolve it and record the responsible person. A mathematical change does not by itself approve equipment capacity, quality acceptance, installation or a purchase decision.
Where do the inputs come from, and which result do they change?
Mark each project value as measured, quoted, taken from a drawing, assumed or awaiting confirmation. Early estimates can use stated assumptions; a missing value is not zero. The calculator defaults are illustrative, not evidence about your plant.
| Input or result / Unit | Evidence to request | Substitution to avoid |
|---|---|---|
| Reference air per bottle (L (reference conditions)) | Ask for per-bottle air use with the bottle format, operating case and declared reference pressure and temperature. Retain the measurement or supplier test basis. | Reference litres and compressed operating volume are not interchangeable. A consumption number without its reference conditions cannot be matched reliably to a compressor supply figure. |
| Bottle rate (Bottles/h) | Identify the counted bottle boundary and the exact observation interval. Retain opening and closing counter readings, accepted quantity and operating mode so the hourly rate can be reproduced. | A machine nameplate rate, instantaneous display and accepted output over a shift are different records. Do not substitute one for another without stating the change of basis. |
Input-to-result trace
The links below trace each input to the equations that use it. They describe mathematical dependence, not every shared input-validation rule. Retain the source, revision, operating condition and person responsible for each value before comparing offers.
Reference air per bottle (L (reference conditions)) → Flow (L/min (reference conditions))
Bottle rate (Bottles/h) → Flow (L/min (reference conditions))
Equations and unit basis
Use the numerical input values in the units shown here. Conversion factors belong to these units. Compare the equation with the calculator result and the example before transferring it to another unit system.
Flow (L/min (reference conditions))
Flow (L/min (reference conditions)) = ((Reference air per bottle × Bottle rate) ÷ 60)
Inputs used in this result: Reference air per bottle (L (reference conditions)); Bottle rate (Bottles/h).
ceil rounds up to a whole count; floor rounds down. min and max select the smallest and largest values. I(P) is 1 when condition P is true, otherwise 0; ∨ means “or”. π is the circle constant. Semicolons separate function arguments.
These relations explain the planning model. A mathematical result does not set acceptance limits, approve a machine setting or establish legal filling tolerances. Keep project approval and evidence separate from arithmetic.
Reference air per bottle + Bottle rate: What happens when two planning inputs change together?
Compare four explicitly hypothetical combinations. Only the two named inputs vary; every other input remains fixed. These examples complete the corner cases around the single-input comparisons above. They are teaching assumptions, not measured plant data, recommended settings, approved limits or probability ranges.
Read A as lower/lower, B as lower/higher, C as higher/lower and D as higher/higher, in the displayed input order. A is the comparison origin, not the original project baseline. The two factors are varied independently for this calculation; that does not prove every combination is physically feasible.
When two multipliers change, adding their percentage changes can miss the cross-effect. Read each result separately: some outputs may use only one of the changed inputs.
Calculated results across the four cases
| Calculated result | A | B | C | D |
|---|---|---|---|---|
| Flow (L/min (reference conditions)) | 768 | 1152 | 1152 | 1728 |
Separate and combined changes from A
| Calculated result | Input or result | Calculated value |
|---|---|---|
| Flow (L/min (reference conditions)) | First input alone: C − A | 384 |
| Flow (L/min (reference conditions)) | Second input alone: B − A | 384 |
| Flow (L/min (reference conditions)) | Both inputs: D − A | 960 |
| Flow (L/min (reference conditions)) | Sum of the two separate changes | 768 |
| Flow (L/min (reference conditions)) | Combined change minus that sum | 192 |
The last difference is D − C − B + A, in the output unit. Zero means the four computed values are additive at these selected points; it does not prove independence in a real line. A nonzero difference can follow from multiplication, division or whole-count rounding. It is not a measured machine interaction or a statistical confidence interval.
Hypothetical combination A: Reference air per bottle = 8 L (reference conditions); Bottle rate = 5760 Bottles/h
Complete inputs for reproducing this case
| Input or result | Calculated value | Unit |
|---|---|---|
| Reference air per bottle | 8 | L (reference conditions) |
| Bottle rate | 5760 | Bottles/h |
Step-by-step substitution from the stated inputs
Intermediate values display up to six decimal places; calculations retain unrounded values. Reproduce operations from the original inputs. Intermediate numbers do not necessarily have the final result unit. π and whole-count functions follow the model reference. CSV numbers use a decimal point.
Flow (L/min (reference conditions))
| Input or result | Operation | Calculated value |
|---|---|---|
| 1 | (8 × 5760) | 46080 |
| 2 | (([Reference air per bottle: 8 L (reference conditions)] × [Bottle rate: 5760 Bottles/h]) ÷ 60) ((8 × 5760) ÷ 60) | 768 |
Hypothetical combination B: Reference air per bottle = 8 L (reference conditions); Bottle rate = 8640 Bottles/h
Complete inputs for reproducing this case
| Input or result | Calculated value | Unit |
|---|---|---|
| Reference air per bottle | 8 | L (reference conditions) |
| Bottle rate | 8640 | Bottles/h |
Step-by-step substitution from the stated inputs
Intermediate values display up to six decimal places; calculations retain unrounded values. Reproduce operations from the original inputs. Intermediate numbers do not necessarily have the final result unit. π and whole-count functions follow the model reference. CSV numbers use a decimal point.
Flow (L/min (reference conditions))
| Input or result | Operation | Calculated value |
|---|---|---|
| 1 | (8 × 8640) | 69120 |
| 2 | (([Reference air per bottle: 8 L (reference conditions)] × [Bottle rate: 8640 Bottles/h]) ÷ 60) ((8 × 8640) ÷ 60) | 1152 |
Hypothetical combination C: Reference air per bottle = 12 L (reference conditions); Bottle rate = 5760 Bottles/h
Complete inputs for reproducing this case
| Input or result | Calculated value | Unit |
|---|---|---|
| Reference air per bottle | 12 | L (reference conditions) |
| Bottle rate | 5760 | Bottles/h |
Step-by-step substitution from the stated inputs
Intermediate values display up to six decimal places; calculations retain unrounded values. Reproduce operations from the original inputs. Intermediate numbers do not necessarily have the final result unit. π and whole-count functions follow the model reference. CSV numbers use a decimal point.
Flow (L/min (reference conditions))
| Input or result | Operation | Calculated value |
|---|---|---|
| 1 | (12 × 5760) | 69120 |
| 2 | (([Reference air per bottle: 12 L (reference conditions)] × [Bottle rate: 5760 Bottles/h]) ÷ 60) ((12 × 5760) ÷ 60) | 1152 |
Hypothetical combination D: Reference air per bottle = 12 L (reference conditions); Bottle rate = 8640 Bottles/h
Complete inputs for reproducing this case
| Input or result | Calculated value | Unit |
|---|---|---|
| Reference air per bottle | 12 | L (reference conditions) |
| Bottle rate | 8640 | Bottles/h |
Step-by-step substitution from the stated inputs
Intermediate values display up to six decimal places; calculations retain unrounded values. Reproduce operations from the original inputs. Intermediate numbers do not necessarily have the final result unit. π and whole-count functions follow the model reference. CSV numbers use a decimal point.
Flow (L/min (reference conditions))
| Input or result | Operation | Calculated value |
|---|---|---|
| 1 | (12 × 8640) | 103680 |
| 2 | (([Reference air per bottle: 12 L (reference conditions)] × [Bottle rate: 8640 Bottles/h]) ÷ 60) ((12 × 8640) ÷ 60) | 1728 |
Use a differing result to identify the joint operating condition that needs evidence. Ask the supplier to check the combination, fixed assumptions and relevant approval before changing equipment. These calculations do not establish acceptance, safe operating ranges or a guaranteed output.
Choose the next planning task
Record simultaneous utility loads, drainage, heat and service access before placing machines. Carry these inputs into the layout review.
Connect this task to the complete line plan
Related planning guides
Request a High- and Low-Pressure Air Network for PET Blowing Scope Review
Share what you know now. The goal is to prepare a useful plant brief before a machine quotation is built.