capacity planning question
How should accumulation be sized between bottling machines?
Accumulation should support selected stop scenarios and controlled recovery without creating product damage, hygiene or quality problems. Simulate real machine behavior, pack stability, controls and available space rather than maximizing conveyor length.
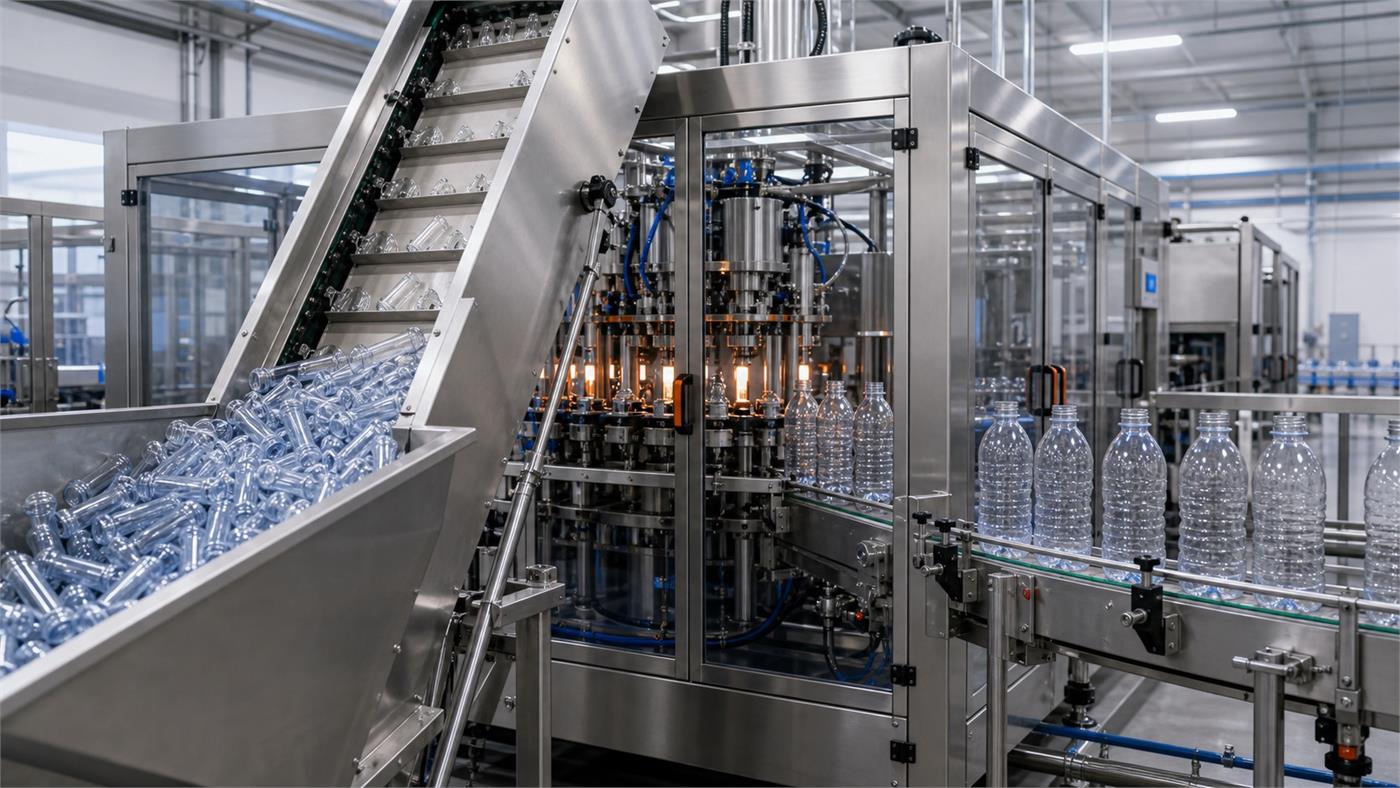
Bottling Line Buffer and Accumulation Sizing
Accumulation should support selected stop scenarios and controlled recovery without creating product damage, hygiene or quality problems. Simulate real machine behavior, pack stability, controls and available space rather than maximizing conveyor length. Use the checklist below to turn the question into a supplier-ready decision without relying on universal figures or unverified claims.
- Machine speed curves
- Stop history or assumptions
- Bottle and pack data
- Factory space
Decisions Behind Bottling Line Buffer and Accumulation Sizing
Define these items against the real product, package, site and production plan before comparing equipment or supplier proposals.
Stop scenarios
Identify upstream and downstream interruptions
Product behavior
Check bottle or pack pressure and dwell
Control zones
Coordinate release and restart
Tradeoffs
Balance uptime support with space and complexity
Bottling Line Buffer and Accumulation Sizing Supplier Evidence Matrix
Use the matrix to separate buyer inputs, supplier commitments and evidence that can be checked during design review, FAT, installation or operation.
| Decision | What to define | Evidence to request |
|---|---|---|
| Stop scenarios | Identify upstream and downstream interruptions | Dynamic line analysis |
| Product behavior | Check bottle or pack pressure and dwell | Control narrative |
| Control zones | Coordinate release and restart | Product accumulation trial |
| Tradeoffs | Balance uptime support with space and complexity | Dimensioned conveyor layout |
Project Inputs for Bottling Line Buffer and Accumulation Sizing
Incomplete inputs force suppliers to make assumptions. Mark unknown items openly and assign the next action instead of hiding the gap.
Machine speed curves
Provide current, project-specific information for bottling line accumulation sizing so the supplier can state assumptions and remaining decisions.
Stop history or assumptions
Provide current, project-specific information for bottling line accumulation sizing so the supplier can state assumptions and remaining decisions.
Bottle and pack data
Provide current, project-specific information for bottling line accumulation sizing so the supplier can state assumptions and remaining decisions.
Factory space
Provide current, project-specific information for bottling line accumulation sizing so the supplier can state assumptions and remaining decisions.
FAQ
How should accumulation be sized between bottling machines?
Accumulation should support selected stop scenarios and controlled recovery without creating product damage, hygiene or quality problems. Simulate real machine behavior, pack stability, controls and available space rather than maximizing conveyor length.
Which inputs are needed for bottling line accumulation sizing?
Start with Machine speed curves, Stop history or assumptions, Bottle and pack data, Factory space. The selected supplier and qualified local specialists must confirm the final project basis.
What evidence should a supplier provide for bottling line accumulation sizing?
Request Dynamic line analysis, Control narrative, Product accumulation trial, Dimensioned conveyor layout. Compare evidence against the same approved product, package, capacity and site conditions.
What is a common mistake when planning bottling line accumulation sizing?
A common mistake is accepting a generic answer without defining the actual bottle, product, output, utilities, interfaces and acceptance method for the project.
How does bottling line accumulation sizing connect to a complete water bottling line?
It affects adjacent equipment, controls, utilities, layout, quality checks or operating responsibilities. Record those interfaces in the complete-line scope and responsibility matrix.
Request a Bottling Line Buffer and Accumulation Sizing Scope Review
Share what you know now. The goal is to prepare a useful plant brief before a machine quotation is built.