conveying integration
PET Bottle Container Conveyor System for a Balanced Water Line
A container conveyor links filling, inspection, labeling and packing while managing bottle spacing, accumulation and controlled stops. The route must fit the actual PET bottle family, machine elevations and line-control philosophy.
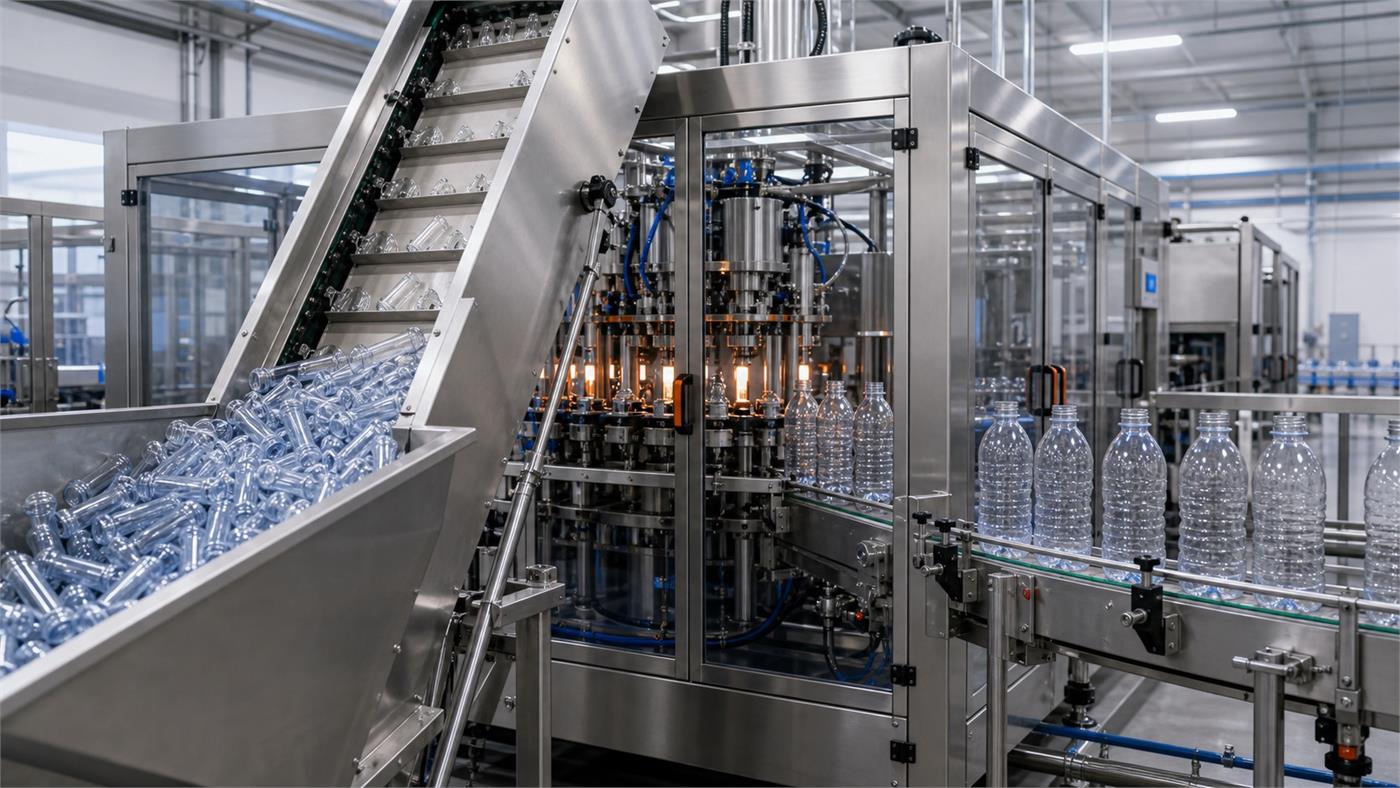
Engineer the Filled-Bottle Route Between Machines
A container conveyor links filling, inspection, labeling and packing while managing bottle spacing, accumulation and controlled stops. The route must fit the actual PET bottle family, machine elevations and line-control philosophy. Use the following decision and evidence framework to compare suppliers on one approved project basis.
- Bottle geometry and base stability
- Machine elevations and transfers
- Buffer and backup control
- Cleaning access and lubrication
Four Decisions for PET Bottle Container Conveyor System
Confirm the package, operating condition, machine interfaces and owner responsibilities before comparing price or delivery.
Bottle support
Confirm base, diameter, height, full weight and every format at all transfers
Route geometry
Coordinate conveyor height, curves, inclines and machine connection points
Control zones
Define sensors, speed control, accumulation and stop propagation between machines
Hygiene and access
Plan drainage, lubrication method, cleaning access, guarding and maintenance removal
PET Bottle Container Conveyor System Supplier Evidence Matrix
Require written evidence for each decision so the item can be integrated into the complete line and accepted under defined conditions.
| Decision | What to define | Evidence to request |
|---|---|---|
| Bottle support | Confirm base, diameter, height, full weight and every format at all transfers | Dimensioned conveyor layout |
| Route geometry | Coordinate conveyor height, curves, inclines and machine connection points | Bottle transfer trial |
| Control zones | Define sensors, speed control, accumulation and stop propagation between machines | Zone-control narrative |
| Hygiene and access | Plan drainage, lubrication method, cleaning access, guarding and maintenance removal | Cleaning and access review |
Project Inputs for PET Bottle Container Conveyor System
These project-specific inputs help suppliers replace assumptions with an engineered and comparable scope.
Bottle matrix
Provide filled samples, drawings and the least stable planned bottle
Machine interface data
Share infeed and discharge heights, directions and signal lists
Production modes
State speeds, changeovers, bypasses and expected accumulation needs
Site constraints
Mark columns, walkways, drains, doors and operator routes
FAQ
What is a PET bottle container conveyor?
It transports bottles between line machines while controlling spacing, accumulation and coordinated machine flow.
How is it different from an air conveyor?
An air conveyor commonly handles lightweight empty PET bottles by the neck; a container conveyor usually supports bottles after filling or at other body-supported stages.
Why are conveyor buffers needed?
Controlled accumulation can absorb short machine interruptions, but its purpose and capacity must be defined for the actual line.
Can one conveyor handle several bottle sizes?
It may, with approved guides, transfers, settings and change parts verified for every bottle.
What should be checked during acceptance?
Check transfers, backup control, restart, bottle stability, changeover, access, guarding and cleaning under representative line conditions.
Request a PET Bottle Container Conveyor System Scope Review
Share what you know now. The goal is to prepare a useful plant brief before a machine quotation is built.