quality integration
Water Bottle Rejection System After Quality Inspection
A rejection system removes identified nonconforming bottles without disrupting the accepted production flow. Selection depends on bottle material, fill state, line speed, defect signal, reject destination and confirmation logic.
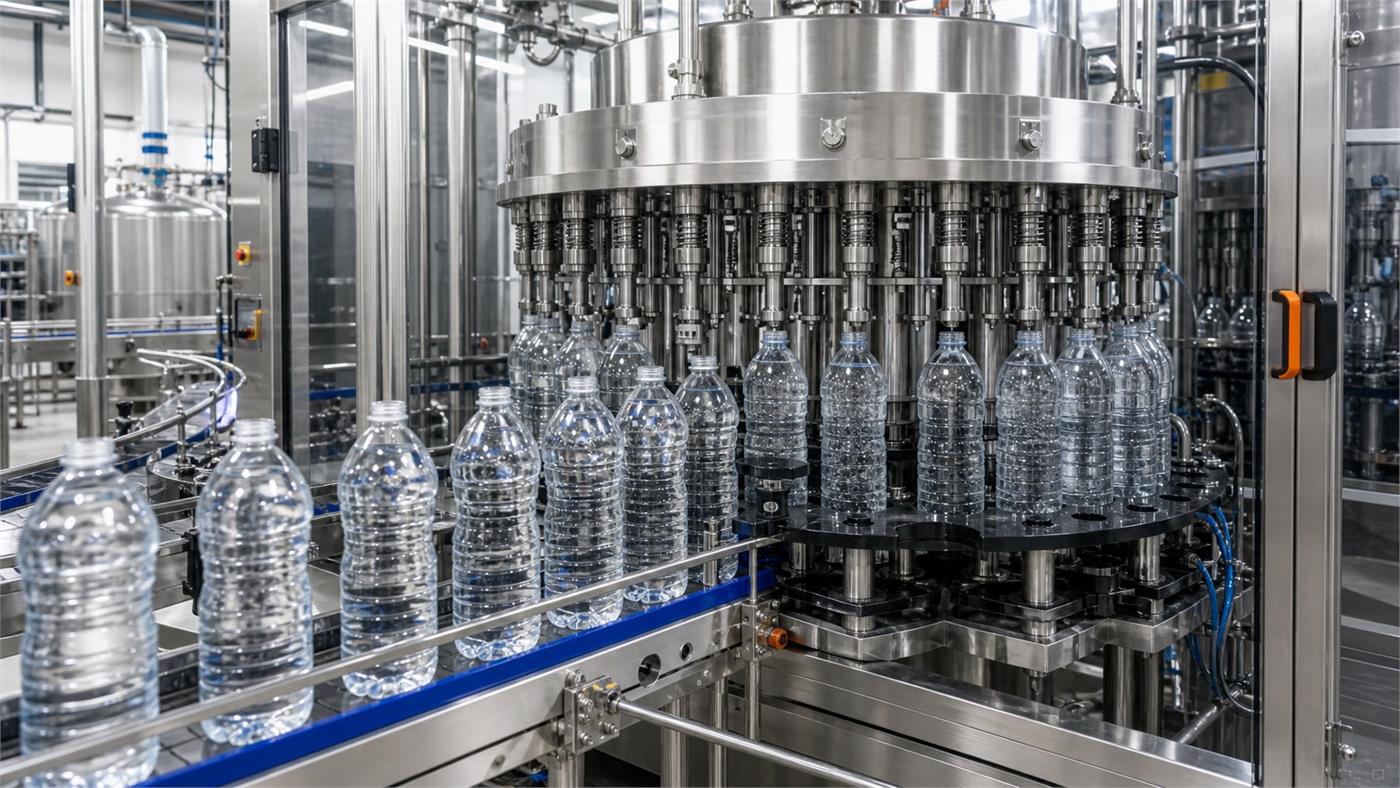
Connect Inspection Decisions to Verified Bottle Removal
A rejection system removes identified nonconforming bottles without disrupting the accepted production flow. Selection depends on bottle material, fill state, line speed, defect signal, reject destination and confirmation logic. Use the following decision and evidence framework to compare suppliers on one approved project basis.
- Defect source and signal timing
- Bottle state and stability
- Reject destination and access
- Confirmation and production records
Four Decisions for Water Bottle Rejection System
Confirm the package, operating condition, machine interfaces and owner responsibilities before comparing price or delivery.
Inspection interface
Define which inspector sends the reject command and how bottle tracking is maintained
Bottle handling
Match the device to empty, full or partly filled PET bottles and the available line gap
Reject destination
Plan a controlled bin, table or parallel conveyor with safe operator access
Verification
Confirm that the commanded bottle leaves the saleable stream and the event is recorded
Water Bottle Rejection System Supplier Evidence Matrix
Require written evidence for each decision so the item can be integrated into the complete line and accepted under defined conditions.
| Decision | What to define | Evidence to request |
|---|---|---|
| Inspection interface | Define which inspector sends the reject command and how bottle tracking is maintained | Inspector-to-reject signal list |
| Bottle handling | Match the device to empty, full or partly filled PET bottles and the available line gap | Bottle handling trial |
| Reject destination | Plan a controlled bin, table or parallel conveyor with safe operator access | Reject area layout |
| Verification | Confirm that the commanded bottle leaves the saleable stream and the event is recorded | Challenge-test and confirmation record |
Project Inputs for Water Bottle Rejection System
These project-specific inputs help suppliers replace assumptions with an engineered and comparable scope.
Rejected bottle samples
Provide the lightest, fullest and least stable formats expected in production
Defect list
State which inspection failures require rejection and whether sorting is needed
Line layout
Share conveyor speed, bottle spacing, available straight length and guarding
Record policy
Define counters, alarms, access and retained quality records
FAQ
What does a bottle rejection system do?
It receives a quality decision and removes the identified bottle from the accepted product flow into a controlled reject route.
Can one rejector handle empty and full PET bottles?
Possibly, but the supplier must verify bottle stability, mass, spacing and the rejection method for each condition.
Where should rejected bottles go?
The project should define a safe bin, table or conveyor that prevents rejected product from returning to the saleable stream.
How is rejection performance tested?
Run known challenge samples and verify detection, tracking, physical removal, confirmation, counters and alarm behavior.
Is the inspector included with the rejector?
Not necessarily. The quotation must separate inspection, tracking, reject hardware, guarding, controls and reject confirmation.
Request a Water Bottle Rejection System Scope Review
Share what you know now. The goal is to prepare a useful plant brief before a machine quotation is built.